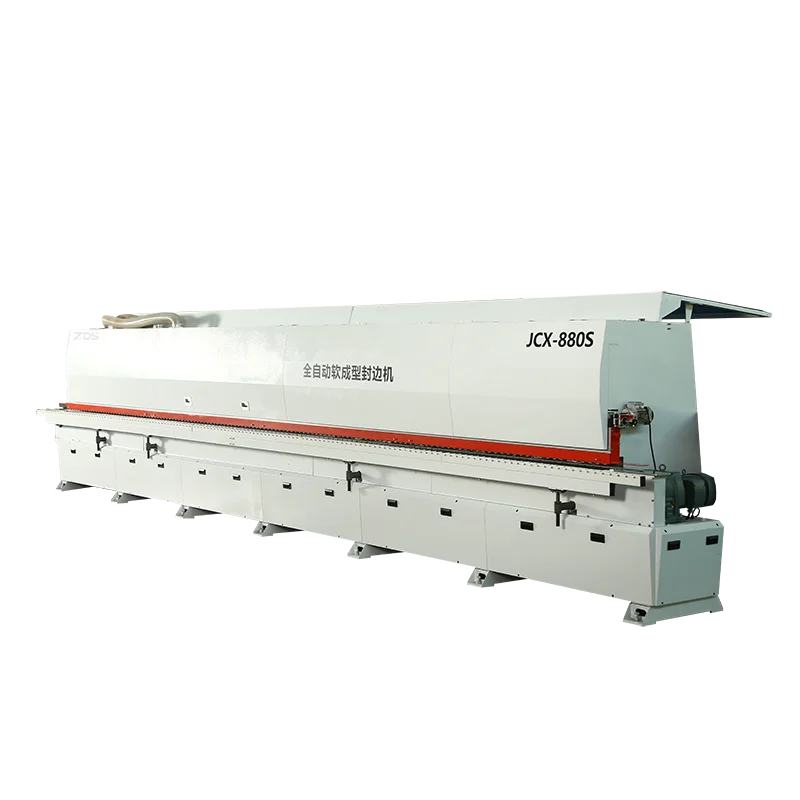
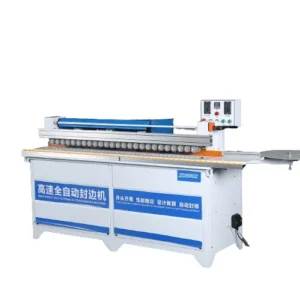
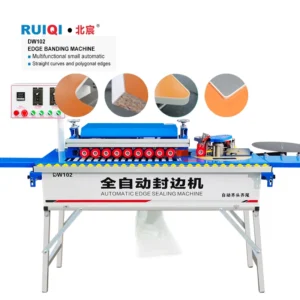
Compact Footprint, Real Output — a soft forming edge bander sized for small workshops moving from manual to machine production, covering 15+ profiles without requiring a full-line investment.
Technical Specifications
| Parameter |
Value |
| Product Type |
Multiple Functional Soft Forming Edge Bander |
| Overall Dimensions |
8.82 × 1.07 × 1.85 m |
| Total Weight |
3200 kg |
| Total Power |
47.1 kW |
| Voltage |
380V |
| Pneumatic Pressure |
0.6–0.8 MPa |
| Panel Thickness Range |
18–22 mm |
| Minimum Sheet Width |
150 mm |
| Minimum Sheet Length |
300 mm |
| Edge Banding Thickness |
0.5–0.8 mm |
| Edge Banding Width |
58 mm |
| Conveying Speed |
6–8 m/min |
| Vacuum Opening Size |
Ф100 × 6 |
| Machining Shapes |
J type, C type, oblique straight, semi-pass, water drop, rhombus, triangle, and 15+ more types |
Application Suitability
| Application |
Material or Output |
| Custom cabinet door profiling |
MDF core with PVC edge banding on contoured edges |
| Small-batch joinery components |
Plywood and particleboard with veneer or PVC trim |
| Furniture panel edge finishing |
Shaped and curved panel edges requiring soft-form profiles |
| Startup workshop production runs |
Mixed-profile jobs with frequent changeovers between batch runs |
Why the Glue Temperature Question Matters More Than Machine Price
Matching the edge banding material to the machine's thermal capacity prevents rework before it happens.
I once specified an entry-level bander for a cabinet door shop transitioning from hand-applied edges. The trial run on PVC strip went smoothly, but once production switched to melamine paper edges, the glue pot could not maintain consistent temperature at the required feed rate. The delamination rate climbed fast enough to scrap an entire batch of door panels. That Soft Forming Edge Bander for small workshop environments taught me to always verify which banding materials a unit actually handles at its rated speed before confirming an order [NEED_CITE: edge banding adhesion standards for thermoplastic and paper-based materials].

Built for Profile Diversity, Not Volume Racing
Small joinery shops rarely run the same profile all day. This soft forming edge bander for small workshop floors supports over 15 edge profiles — J, C, oblique, water drop, rhombus, triangle — meaning a single unit covers the majority of contoured edge work a custom furniture maker encounters. Changeover between profiles is a routine adjustment rather than a full reconfiguration, which keeps downtime manageable when batch sizes stay small.
Minimum Sheet Dimensions That Reflect Real Offcuts
The 150 mm minimum width and 300 mm minimum length are not arbitrary numbers pulled from a brochure. In a cabinet shop, offcuts and narrow stile components regularly fall below standard panel sizes. A machine that cannot grip a 150 mm strip forces operators to edge-band oversized blanks and trim afterward, adding a secondary operation and wasting material. This unit accepts those smaller workpieces directly [NEED_CITE: common panel dimensions in custom cabinet manufacturing].
How Feed Speed and Glue Pot Capacity Interact
The 6–8 m/min conveying speed sits at the lower end of the industrial spectrum, and that is deliberate for this machine class. At higher feed rates, the glue pot must replenish heat faster to maintain the adhesive at its working temperature across the entire contact zone. For a 47.1 kW total power allocation shared across all stations — milling, gluing, pressing, trimming — this feed speed ensures the glue zone does not starve thermally when processing PVC or veneer stock at 0.5–0.8 mm thickness. Pushing the speed beyond this range with heavier adhesive demands risks cold joints, especially on MDF substrates that absorb heat from the glue line faster than plywood does. The 18–22 mm panel thickness range aligns with standard furniture board stocks, meaning the pressure rollers and glue roller maintain consistent contact without requiring manual gap adjustments between common thicknesses.
The Cost of Ignoring Voltage and Frequency Upfront
Shipping a 380V machine to a workshop running 220V three-phase without confirming compatibility beforehand is a surprisingly common failure. The motor windings on a unit like this are wound for a specific supply; running it on the wrong voltage either overheats the motor or starves the glue pot heater. Either outcome surfaces weeks after installation, not during the factory test. Buyers who skip this verification step end up paying for rewinding or replacement transformers on top of the original freight cost [NEED_CITE: international voltage and frequency standards for industrial woodworking machinery].
Why Sourcing This Configuration Makes Sense
The four-stage quality control process — incoming material inspection, in-process checks, finished product verification, and pre-shipment testing — applies to this soft forming edge bander before it leaves the factory floor. Voltage and control panel language are confirmed before production starts, not discovered after the crate arrives. The patented cutting mechanisms deliver verified tolerances on profile trimming, which matters when shaped edges must mate with adjacent panels during assembly. Engineer-led configuration recommendations arrive within 24 hours of inquiry, so you can confirm whether this unit fits your current profile mix before committing. Factory visits are available for buyers who want to see the machine running their actual substrate and edge material before signing off [NEED_CITE: ISO 9001 quality management requirements for machinery manufacturers].
Documentation & Verification
- CE declaration of conformity covering machinery directive compliance for this edge bander class
- ISO 9001 certificate documenting the quality management system behind production
- Machine specification sheet confirming panel thickness range, conveying speed, and profile capabilities
- Electrical schematic with voltage and frequency confirmed for your local supply before dispatch
- Factory test record on your specified edge banding material and profile shape before shipment
- Operation and maintenance manual written in your operator's working language
Installation, Commissioning & Support
- Floor space of approximately 9 × 1.5 meters with clearance for operator access on the feed side
- Dedicated 380V three-phase circuit rated for the 47.1 kW total power draw plus startup surge
- Machine ships partially assembled; final station alignment and belt tensioning completed on-site
- First-run commissioning includes glue temperature mapping across PVC and veneer at your feed speed
- Six vacuum ports (Ф100) require connection to existing dust extraction or a dedicated collector
- Spare parts list covers wear items: glue roller, trimming blades, pressure roller surfaces
What to Share Before Requesting a Quote
Send your typical edge banding material — PVC, veneer, or melamine paper — along with the thickness and width you run most often. Confirm your workshop's voltage and frequency so the electrical system can be configured before build. If you have a profile sample or a drawing of the shaped edge you need, include that so the machining stations can be verified against your actual work.
Frequently Asked Questions
Q: Is this soft forming edge bander the right size for my workshop volume and floor space?
A: The unit occupies roughly 8.82 × 1.07 meters and weighs 3200 kg, fitting into workshops that lack the space for a full production line. Its 6–8 m/min feed speed suits small-batch, multi-profile work rather than continuous high-volume output. If your daily runs involve frequent profile changes on cabinet components and joinery pieces, this configuration matches that workflow without overcommitting floor area or power infrastructure.
Q: What voltage does the machine require, and can it be set up for my local supply?
A: The standard configuration runs on 380V three-phase power. Before production begins, your local voltage and frequency are confirmed so the motor windings, control transformer, and glue pot heaters are matched to your actual supply. This verification step prevents motor overheating and adhesive temperature failures that surface only after installation in workshops with incompatible power infrastructure.
Q: Which edge profiles and materials does it handle?
A: The machine covers over 15 profiles including J, C, oblique straight, semi-pass, water drop, rhombus, and triangle shapes. It processes PVC and veneer edge banding at 0.5–0.8 mm thickness and up to 58 mm width. Switching between profiles involves adjusting the machining stations for the specific shape, and the minimum sheet dimensions of 150 × 300 mm allow small components to be processed directly.
Q: What happens when my production volume grows beyond this machine?
A: This unit is designed as an entry point into mechanized soft-form edge banding. As volumes increase, workshops typically add dedicated straight-line edge banders or higher-speed contour machines alongside it rather than replacing it. The original machine continues handling specialty profiles and short runs while newer equipment absorbs the repetitive high-volume work.
Q: How is installation handled once the machine arrives?
A: The machine ships with assembly documentation and arrives partially assembled. Final station alignment, belt tensioning, and glue pot calibration are completed on-site. Commissioning includes running your actual edge banding material on your chosen profile to verify adhesion and trim quality. An operation and maintenance manual in your language covers daily startup, consumable replacement, and troubleshooting procedures.